
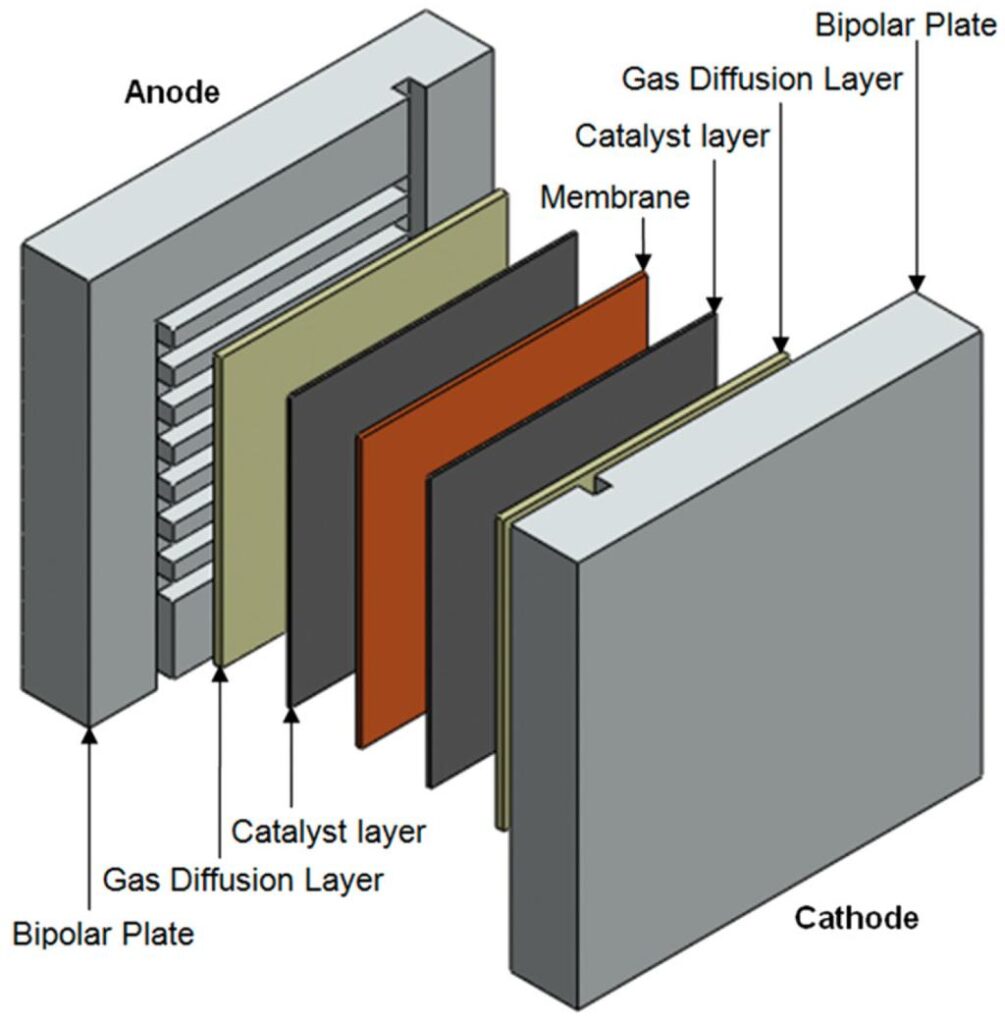
Graphite bipolar plates are graphite-based components that conduct current between cells and provide fluid-distribution and separation features. In a proton exchange membrane fuel cell, the main electrochemical reactions occur in the catalyst layers, rather than on the bipolar plate itself.
Manufacturing depends on the material system. A plate machined from graphite stock follows a different route from a graphite-polymer composite formed in a mold. Understanding that distinction helps connect material descriptions, processing steps and finished-part acceptance.
Key takeaway: Specify the graphite system, preparation route and delivered condition together. Then verify the finished plate under its intended operating and assembly conditions.
What Material Systems Are Used in Graphite Bipolar Plates?
Graphite Stock for Machined Plates
Machined plates begin with a specified graphite grade and treatment state. For example, isostatic pressing describes a method of forming graphite stock. It does not, by itself, define the finished plate’s geometry, impregnation or acceptance requirements.
Graphite-Polymer Composites
Graphite-polymer plates combine a conductive carbon filler with a polymer binder. Fuel-cell compound development includes graphite and other carbon-based fillers, with formulations matched to their production routes.
For graphite-filled plates, identify both the filler and binder. “Graphite composite” alone leaves important manufacturing inputs unspecified.
Expanded and Flexible Graphite-Based Systems
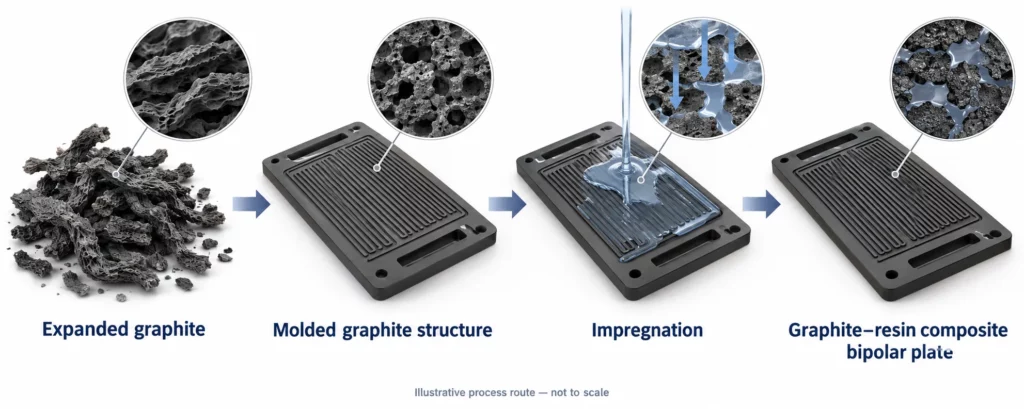
Expanded graphite can form part of a polymer composite or a sheet-based structure. An expanded-graphite/resin plate route can involve forming, impregnation and curing.
These descriptions refer to different classification dimensions:
| Term | What it identifies | What remains to be specified |
|---|---|---|
| Natural or synthetic | Graphite source | Grade, composition and processing state |
| Isostatic graphite | Stock-forming method | Treatment and finished-part requirements |
| Impregnated graphite | Treatment state | Impregnant, process stage and verification |
| Graphite-polymer composite | Material composition | Binder, filler and forming route |
| Expanded or flexible graphite | Material form or sheet structure | Composite construction and treatment |
One product may fit several descriptions. Avoid treating every term as a separate, mutually exclusive material family.
How Are Bipolar Plates Made from Graphite Stock?
Define the Starting Grade and Treatment State
Start with the qualified blank: its grade, dimensions, material condition and traceability.
Upstream synthetic graphite production can include powder preparation, forming, baking and graphitization. A manufacturer machining purchased graphite stock starts after those upstream operations.
Keep the stock specification separate from the finished-plate drawing. Approval of the starting material does not establish that its machined channels or sealing surfaces meet the component requirements.
Machine the Flow Field and Functional Areas
Machining translates the drawing into channels, ports, sealing regions and assembly references. Establish the datums used to locate these features and the sections used to measure channel width and depth.
Review the remaining material around channels, holes and edges. Define inspection for local damage and dimensional conformity, particularly where a feature interfaces with a seal or neighboring component.
The useful output is a plate linked to its drawing and inspection results. A description such as “precision-machined graphite” provides little acceptance information on its own.
Verify Impregnation, Finishing and Cleaning Requirements
Where impregnation is required, identify the treatment and its place in the route. Pitch impregnation during stock production and resin treatment of a graphite-based plate should be distinguished.
Confirm whether subsequent machining or finishing changes the surfaces that require verification. Define cleaning and the delivered condition before testing.
Use a qualified sequence for the selected grade and treatment. A universal impregnation time or fixed processing order would omit these material-specific decisions.
How Are Graphite-Polymer Composite Bipolar Plates Formed?
Compression Molding
Compression molding shapes a prepared compound under pressure in a mold. The binder determines how that shape becomes stable.
For a thermosetting route, epoxy/expanded-graphite composites can be hot-molded and post-cured. Curing creates the polymer network that holds the composite together.
Thermoplastic processing instead uses heating and subsequent solidification. Keep those mechanisms distinct when defining temperature, pressure, release and post-processing conditions.
Review the molded plate after release. Check the specified geometry and functional surfaces in the delivered state, rather than accepting it from the mold settings alone.
Injection Molding
Injection molding must accommodate the compound’s flow and solidification behavior. High graphite loading can improve conductivity while making the melt more difficult to process.
Injection-compression molding of graphite-filled polypropylene combines material injection with controlled compression and mold-temperature management. Filling capability and thickness consistency must be evaluated together.
For a proposed geometry, define the flow distance, wall sections and required feature detail. Confirm these on representative molded parts. Successful filling of a simple specimen does not establish that every thin channel or large plate can be reproduced.
Binder Retention and Post-Processing
Some composite plates retain their polymer binder as part of the finished material. Polypropylene-based and cured epoxy-based plates therefore require different processing descriptions from carbonized or graphitized products.
Do not add binder removal and graphitization as automatic steps after molding. Establish the intended final material first.
Any trimming, finishing or surface treatment should then have a defined purpose and acceptance check. For the wider relationship between material systems and production stages, see the bipolar plate manufacturing process.
How Does Preparation Affect Finished-Plate Performance?
Preparation affects more than the visible channel pattern. Formulation, forming and treatment must be connected to the properties that the finished component needs.
For example, epoxy/expanded-graphite formulation and dispersion influence electrical and mechanical results. Increasing graphite content should therefore be evaluated as a formulation change, rather than assumed to improve every property.
Use the following review framework:
| Preparation issue | Finished-part checks to define |
|---|---|
| Porosity, impregnation and forming defects | Gas permeability or leakage under specified conditions |
| Filler, binder and forming state | Electrical direction, surface condition and contact behavior |
| Channels, edges and remaining sections | Geometry and mechanical integrity |
| Material and treatment state | Stability under the intended medium and temperature |
Separate in-plane conductivity, through-plane conductivity and contact resistance. They describe different electrical paths. Keep measurement direction, contact material and loading conditions with the reported result.
Likewise, low porosity or an intact-looking surface does not demonstrate compliance with a project’s leak limit. Define the test boundary and acceptance conditions separately.
The bipolar plate requirements and test methods provide a further reading path for planning these evaluations.
Surface Processing, Wettability and Water Management
Laser processing needs a defined material and pulse regime. Nanosecond processing of graphite composites should not be relabeled as evidence for ultrafast laser processing.
Laser-induced hydrophilic surface methods have also been disclosed for graphite-containing materials. A method disclosure does not establish production durability.
Evaluate water contact angle alongside surface integrity, electrical contact and relevant cell operation. A more hydrophilic surface alone does not establish improved PEMFC water management or efficiency.
Which PEM Fuel Cell Conditions Need Separate Validation?
Match the material, binder and impregnation system to the intended temperature, fluids, pressures and assembly contact conditions.
Low-temperature PEMFC approval should not be transferred automatically to high-temperature PEM operation. Injection-molded plates developed for HT-PEM use an application-specific compound and process supported by cell-level testing.
For the project, define which exposure and assembly conditions the evidence must represent. Identify whether a result concerns a material coupon, a plate or an operating cell.
When formulation or post-treatment changes, review the affected validation requirements before carrying the previous approval forward.
What Should a Graphite Bipolar Plate Specification Include?
Prepare a specification that connects the material description to measurable finished-part requirements:
- Grade or formulation identification;
- Binder, impregnation and treatment state;
- Drawing revision, channels, sealing zones and datums;
- Electrical measurement direction and contact conditions;
- Operating media, temperature and pressure range;
- Gas-test boundary, conditions, limit and units;
- Inspection coverage and specimen or component identity.
Keep the approved material and process state with the inspection records. This prevents a result from one formulation or specimen geometry being presented as approval for a different finished plate.
TMNetch Case: Defining Acceptance by Functional Area
In a separate TMNetch photo-etching order, a customer questioned small connection points around the parts. The factory explained that these kept the parts attached to the production sheet and could be made smaller where processing allowed.
The customer accepted them provided they did not affect the functional area. This documented retaining-tab order was a metal-etching acceptance case, not a graphite-production case.
The transferable lesson is to define permitted conditions by location and function. For graphite specifications, identify the relevant channel, sealing and contact regions and their acceptance requirements.
FAQs
Are all graphite bipolar plates made by machining?
No. Machining graphite stock, molding graphite-polymer compounds and forming graphite-based sheet structures are different routes. Identify the material system before describing its manufacture.
Do graphite-polymer plates need graphitization after molding?
Not as a universal step. Some plates retain a thermoplastic or cured thermosetting binder. Define the intended finished composition and its required post-processing.
Are graphite bipolar plates the same as graphite electrodes?
The terms are not interchangeable. In a PEMFC, the bipolar plate provides electrical connection and fluid-distribution boundaries, while the principal electrode reactions occur in the catalyst layers.
Conclusion
A graphite bipolar plate specification should connect the material system, preparation route and finished-part evidence. Evaluate the actual component under its intended operating and assembly conditions.
If comparing graphite with other material families, use the material selection guide to review the tradeoffs on a consistent basis.