
The dimensions of a bipolar plate flow channel cannot be selected independently. Channel width, channel depth and rib width work as one geometric system. Changing one dimension can alter gas velocity, pressure drop, transport through the gas diffusion layer, GDL compression and electrical contact at the plate–GDL interface.
For this reason, a channel that improves reactant transport may also require a higher pressure differential or change the mechanical support provided to the GDL.
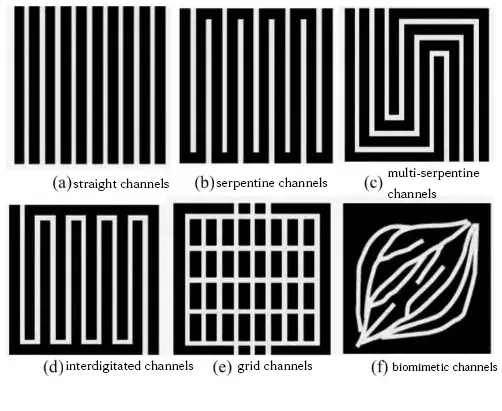
This guide focuses on these dimensional relationships in conventional low-temperature proton exchange membrane fuel cells, or PEMFCs. Anode and cathode conditions should be evaluated separately. Different flow-field layouts—such as parallel, serpentine or interdigitated designs—create their own transport characteristics. For layout selection, see our guide to types of bipolar flow channel design.
Here, the question is narrower:
Once a general flow-field layout has been selected, how do channel width, depth, rib width, length and path count affect the design?
Key Takeaways
Define exactly which dimension is being changed before comparing two designs.
Compare gas velocity, pressure requirement, GDL transport and electrical contact together.
Do not treat a single experimental “optimal dimension” as a universal design rule.
Separate nominal CAD dimensions from the cross-section that can actually be manufactured and inspected.
Evaluate channel geometry under defined gas-side, load, humidity, compression and flow conditions.
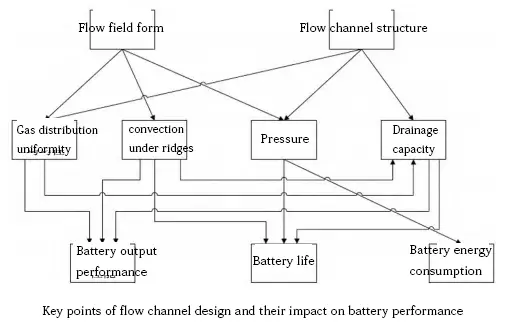
Define Channel Width, Depth and Rib Width Before Comparing Designs
Before running CFD, comparing test data or sending a bipolar plate drawing for manufacturing, establish a consistent definition for each dimension.
Channel Width, Channel Depth and Rib Width
For a typical repeating flow-field section:
| Dimension | Recommended Drawing Definition |
|---|---|
| Channel width, w | Opening width measured at the specified section or reference plane |
| Channel depth, h | Distance from the plate reference surface to the channel floor |
| Rib width, r | Width of the land between adjacent channels |
| Pitch, p | Repeat distance from one channel to the next |
| Remaining metal thickness | Metal remaining below or between etched features |
For equal repeating straight channels:
p = w + r
The local channel-to-land ratio can therefore be written as:
w / r
The projected open-channel fraction in this repeating section is:
w / (w + r)
This value is useful for describing the plate geometry, but it should not be confused with GDL porosity. GDL porosity describes void space inside a porous material. The projected opening fraction of a flow field does not directly define the total electrochemically active area.
Define the Comparison Baseline First
A statement such as “the narrower channel performed better” is incomplete unless the comparison conditions are known.
Before evaluating candidate dimensions, record at least:
| Input | What Should Be Defined |
|---|---|
| Geometry | Flow-field layout, active area, channel length and number of parallel paths |
| Gas conditions | Electrode side, temperature, pressure and humidity |
| Gas supply | Flow rate or stoichiometric ratio |
| Electrical load | Cell voltage or current density |
| GDL interface | GDL material, thickness and compressed condition |
Stoichiometric ratio describes the relationship between reactant supplied to the cell and the reactant required by the electrochemical reaction.
If the electrical load changes during a test, determine whether the supplied reactant flow changes at the same time. Otherwise, an apparent geometric improvement may partly result from a different operating condition.
How Channel Width and Depth Affect Gas Velocity
For a defined flow condition, reducing the channel cross-sectional area increases mean velocity.
The basic continuity relationship between flow, area and velocity gives:
u_mean = Q_ch / A
For an ideal rectangular channel:
A = w × h
where:
u_mean = mean channel velocity
Q_ch = volumetric flow through the channel
w = channel width
h = channel depth
For N identical parallel flow paths receiving equal flow:
u_mean = Q_total / (N × w × h)
This relationship explains an important design point.
If total flow, channel depth and path count stay unchanged, reducing channel width increases mean velocity.
But if the number of parallel paths also changes, the comparison is no longer equivalent because the flow through each individual channel changes.
In an operating PEMFC, the calculation becomes more complex because local gas flow can change along the flow path as reactants are consumed and water is produced.
Channel Width Changes More Than Velocity
Narrowing a channel does not automatically mean better cell performance.
A smaller channel opening changes:
local gas velocity,
hydraulic resistance,
pressure distribution,
liquid-water transport,
and the relative width of the neighboring ribs.
These effects must be considered together.
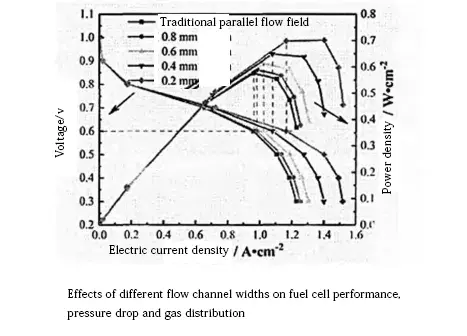
The important information in this figure is not that one width should always be selected. It demonstrates that channel width is capable of changing the cell response and therefore needs to be evaluated under the intended operating conditions.
Why Shallower Channels Can Require More Pressure
Channel depth has a particularly strong influence on hydraulic resistance.
For a rigid, straight channel that is much wider than it is deep, a simplified laminar-flow relationship can be written as:
Δp ≈ 12 × μ × L × Q_ch / (w × h³)
where:
Δp = pressure drop
μ = dynamic viscosity
L = channel length
Q_ch = volumetric channel flow
w = channel width
h = channel depth
This approximation assumes steady, fully developed, incompressible, single-phase laminar flow. It is useful for understanding sensitivity, not for predicting every PEMFC flow field.
Because depth appears approximately as h³ in this simplified relationship, relatively small changes in depth can produce a much larger change in hydraulic resistance.
For example, if channel depth is reduced by 20% while other variables remain fixed:
mean velocity increases by approximately 25%
the simplified pressure-drop estimate becomes approximately:
1 / 0.8³ ≈ 1.95
or nearly twice the original value.
Actual PEMFC channels require a more complete treatment because gas compressibility, bends, reaction, liquid water, channel shape and GDL interaction may all influence the pressure field.
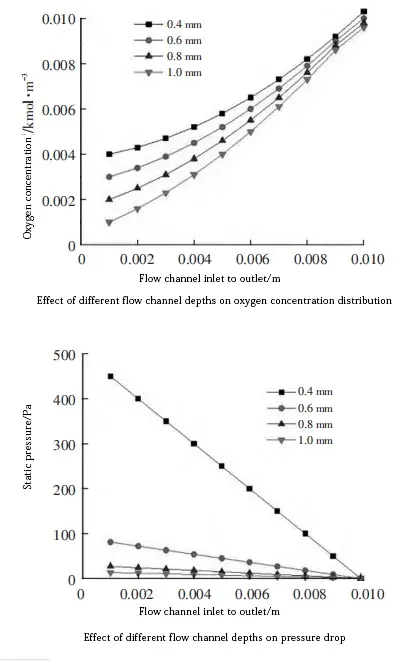
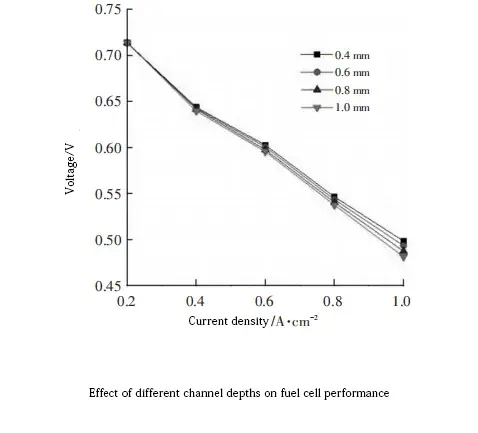
This distinction is important. A depth such as 0.6 mm can be a valid candidate for a specific plate, experiment or simulation. It should not become a general PEMFC design rule unless the corresponding geometry, GDL, flow conditions, load and objective are also specified.
Higher Velocity Does Not Automatically Mean Higher Net Performance
Increasing velocity can support water removal and reactant transport in some operating regimes, but that does not by itself prove that the design is better.
The blower or compressor must provide the required pressure.
At the same time, water distribution inside the channel and GDL changes oxygen access to the catalyst layer. Experimental and numerical studies have shown that water location and under-rib transport influence oxygen transport.
A meaningful comparison therefore needs to consider both:
cell-level output
and
the pressure required to deliver the reactant flow
rather than using velocity alone as the optimization target.
Rib Width Connects Gas Transport with the GDL Interface
The rib—also called the land—is the solid region between two neighboring channels.
Reactant does not flow directly through the metal rib. Gas must reach catalyst regions beneath the rib by moving through the porous GDL.
This can involve diffusion as well as pressure-driven under-rib convection.
Reducing rib width shortens the lateral transport distance beneath the land. However, changing rib width also changes the mechanical and electrical interface between the bipolar plate and GDL.
That produces an important design trade-off.
Narrower Ribs Can Change Under-Land Transport
A narrower rib can reduce the distance reactant must travel beneath the land.
Whether that improves cell behavior also depends on:
GDL permeability,
local water accumulation,
pressure differences between neighboring channels,
and GDL compression.
The area covered by the ribs should not simply be treated as inactive catalyst area.
Rib Width Also Changes Compression and Electrical Contact
The channel-and-rib pattern produces nonuniform compression in the GDL.
Regions below a rib experience different mechanical conditions from regions beneath an open channel.
Compression can improve electrical contact while simultaneously reducing gas permeability.
Similarly, electrical contact resistance varies across the plate–GDL interface.
For this reason, the nominal rib area alone is not sufficient for judging electrical performance.
A design review should also define:
stack clamping condition,
GDL specification,
bipolar plate surface condition,
rib contact width,
and expected compression.
Do not retain the old text claiming that a universal 40–75% “porosity” range is required. In this article, use the image only to explain the channel-to-land geometry.
Use Channel Area Fraction as a Geometric Parameter
The channel opening fraction is useful for describing a CAD pattern:
w / (w + r)
but it should remain a geometric parameter.
For example:
| Geometry Change | Mechanism to Review | Related Checks |
|---|---|---|
| Narrower rib at fixed channel width | Shorter under-rib transport distance and changed contact pattern | GDL permeability, compression and local pressure |
| Wider channel at fixed pitch | Larger opening fraction and narrower supporting land | GDL intrusion, contact area and mechanical support |
| Higher GDL compression | Changed electrical interface and permeability | Gasket condition, stack force and GDL response |
There is no reason to select a channel-to-land ratio using opening percentage alone.
Channel Length Directly Changes the Hydraulic Comparison
Channel dimensions must also be evaluated together with path length.
For otherwise similar straight channels, frictional pressure loss increases as the flow path becomes longer.
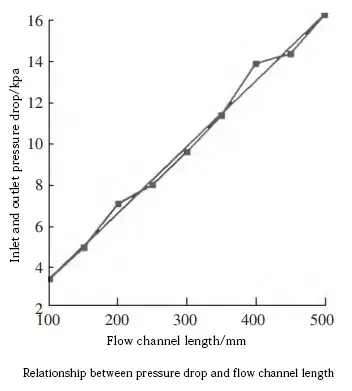
Avoid retaining the old statement that pressure drop universally rises by a fixed number of kilopascals for every 50 mm. The image is still valuable for illustrating the length effect.
Bends and Complete Flow-Path Geometry Also Matter
A serpentine flow field introduces bends in addition to straight-channel friction.
Therefore, two designs cannot be compared using channel cross-section alone.
The comparison should include:
total path length,
width and depth,
number and geometry of turns,
number of parallel paths,
and flow through each path.
Research also shows that serpentine geometry and path count can alter pressure requirements and pumping losses.
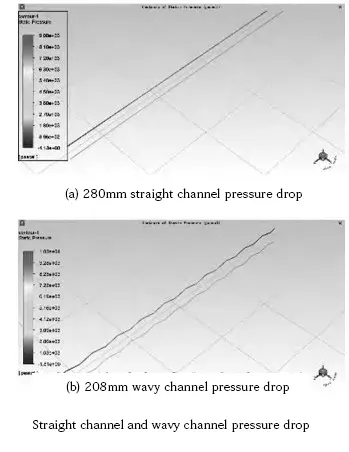
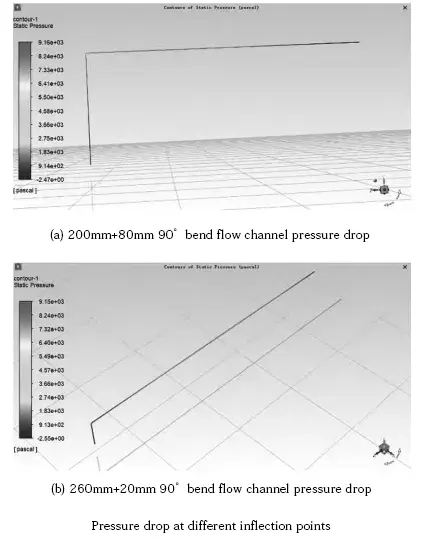
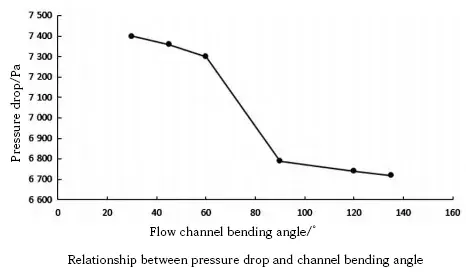
These figures can all remain on the page, but they should support the broader point: complete path geometry controls resistance. They no longer need separate sections claiming universal performance advantages for different channel forms.
More Parallel Paths Change Flow per Channel
Parallel-path count is another variable that can invalidate an otherwise simple width comparison.
If total supplied flow remains fixed and is divided equally between N identical channels:
Q_ch = Q_total / N
Increasing the number of parallel flow paths therefore reduces the nominal flow through each path.
However, real flow distribution may not be perfectly equal.
Manifold geometry, inlet regions and differences in downstream resistance can produce uneven path-to-path supply.
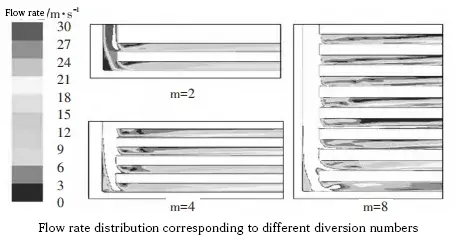
The figure should no longer be used to claim that a particular split number is universally best.
Include Manifolds and Distribution Zones in the Comparison
Channel performance also depends on how gas reaches the individual flow paths.
Ports, manifolds and transition regions can alter inlet distribution before the reactant enters the main flow field.
For designs where distribution is critical, review the ports, manifolds and fluid-isolation structure of the bipolar plate together with the channel dimensions.
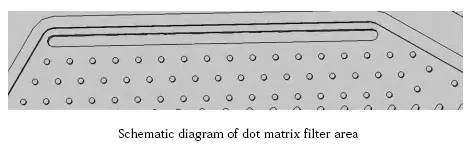
This is a much better fit for the existing transition-zone illustration than retaining a broad section about bipolar plate inlet and outlet theory.
How to Interpret an “Optimal” Channel Dimension
Published papers and simulation studies frequently report an “optimal” width, depth or channel-to-rib ratio.
That number should always be read together with its experimental or numerical conditions.
For any proposed optimum, retain at least the following information:
| Evidence Item | Information Required |
|---|---|
| Geometry | Layout, active area, width, depth, rib width, length and number of paths |
| Operating conditions | Electrode side, temperature, pressure, humidity, reactant supply and load |
| Model assumptions | Single- or multiphase treatment, thermal assumptions and GDL model |
| Interface condition | GDL material and compression |
| Objective | Current density, power, pressure drop, efficiency or another target |
| Evidence type | Simulation, experiment or both |
| Traceability | Original figure, table and study |
For example, channel and rib dimensions interact with operating conditions and electrical losses.
A value obtained from one optimization study is therefore a conditional result, not a general drawing standard.
If the conditions behind a recommended value cannot be recovered, it is safer not to present that value as a design recommendation.
Separate a Dimensional Trend from a Validated Design
A dimensional trend can help narrow the design space.
It cannot replace validation.
Once candidate width, depth and rib dimensions are identified, use CFD and prototype validation to determine whether the complete plate behaves as intended.
Validation should reproduce the geometry and operating conditions that matter for the intended stack rather than only verifying the nominal channel dimensions.
Turn the Designed Channel into a Manufacturable Metal Plate
A simulated rectangular channel and a manufactured metal channel are not necessarily identical.
In chemical etching, lateral material removal can create undercut, tapered walls and rounded transition features. General photochemical machining guidance therefore supports specifying the required manufactured section rather than assuming an idealized rectangular groove.
For an etched bipolar plate, a design review may need to define:
channel opening width,
floor width,
channel depth,
rib-top contact width,
remaining metal thickness,
feature position,
and measurement plane.
For double-sided channels or multi-depth structures, specify the positional relationship between features on both sides of the sheet.
Channel cross-sectional shape itself can also influence cell behavior, so the geometry used in analysis should represent the geometry the manufacturing process can realistically produce.
For practical manufacturing limits, see our chemical etching design guidance for bipolar plate flow channels.
TMNetch Manufacturing Example: Define Functional Areas on the Drawing
A useful drawing lesson comes from a previous TMNetch photo-etched component order involving retaining tabs.
The customer questioned several small connection points remaining on the part. These were intentional retention features used during processing and could be reduced when manufacturing conditions allowed. The customer accepted them as long as they remained outside the functional area.
The same principle is useful when releasing an etched bipolar plate.
Clearly identify:
functional channel openings,
rib contact surfaces,
sealing regions,
dimensional inspection zones,
and areas where temporary retention features are permitted.
Instead of writing only “must not affect function,” convert the requirement into explicit feature-location and acceptance criteria.
Frequently Asked Questions
What Channel Depth Is Best for a PEM Fuel Cell?
There is no universal channel depth for all PEMFC designs.
Select depth according to the electrode side, flow condition, channel geometry, GDL state, pressure requirement and optimization objective. Any recommended depth should remain linked to the conditions under which it was validated.
Is a Higher Channel-to-Land Ratio Always Better?
No.
Increasing the channel opening fraction changes the under-rib transport distance, GDL support, compression and electrical contact at the same time.
Evaluate these effects together rather than optimizing the opening fraction alone.
Do Narrower Channels Always Improve Fuel Cell Performance?
No.
At fixed depth, path count and flow per path, a narrower channel increases mean gas velocity. It also changes hydraulic resistance and wet-operation behavior.
The design should therefore be assessed using pressure requirement, gas distribution, water management and measured cell performance.
Does Channel Length Matter If Width and Depth Stay the Same?
Yes.
Longer paths generally increase frictional pressure losses. Bends and other geometric changes add additional resistance, so the complete flow path should be included in the comparison.
Review Bipolar Plate Channel Dimensions Before Releasing the Drawing
Channel width and depth define the gas passage. Rib width connects the flow field to GDL transport, mechanical support and electrical contact. Channel length and parallel-path count determine the hydraulic baseline around those dimensions.
For that reason, a bipolar plate dimension should not be described only as “0.5 mm wide” or “0.6 mm deep.”
A useful specification defines both:
the geometry
and
the operating conditions under which that geometry was selected.
If you are preparing custom etched bipolar plates, send TMNetch the material, sheet thickness, channel section, rib dimensions, critical tolerances and required inspection locations.
We can review whether the proposed geometry can be manufactured and measured before the drawing is released for chemical etching.